Private Label Visual Timer Quality Control: Factory Checks That Prevent Defects and Inconsistent Performance
- Build a factory inspection plan for visual countdown devices
- Convert the product specification into testable criteria
- Inspect incoming materials and critical components
- Use lot sampling with clear acceptance rules
- Verify timing, display behavior, and operating reliability
- Measure countdown accuracy across the operating range
- Check visibility, controls, sound, and power behavior
- Use standards appropriately and compare test methods
- Turn inspection results into stronger supplier and brand outcomes
- Define nonconformance handling before production
- Connect quality controls to product range and production planning
- Evaluate the evidence behind every quality claim
- Frequently Asked Questions
Reliable private-label visual timer quality starts with a defined inspection plan, not a final glance at finished units. Buyers should verify component quality, countdown accuracy, visual indication, controls, alarms, power performance, and packaging at appropriate stages of production. A documented combination of incoming inspection, in-process checks, functional testing, and lot-level acceptance helps prevent recurring defects and inconsistent user experiences. Clear specifications, traceable test records, and corrective-action procedures also make supplier performance easier to evaluate before a product reaches retail or institutional users.
Build a factory inspection plan for visual countdown devices
A timer can appear well made while still failing in daily use: its colored disk may move unevenly, the countdown may drift, a button may stick, or the alarm may be too quiet for the intended setting. Quality control should therefore translate the product brief into measurable acceptance criteria before mass production begins. The control plan should identify what is checked, how it is measured, how often it is checked, who records the result, and what happens when a result falls outside limits.
Convert the product specification into testable criteria
Start by documenting the intended timing range, the accuracy tolerance across that range, the display behavior, alarm options, control response, power source, and operating environment. Define the conditions for each test, including the timer setting, observation period, measurement instrument, and pass/fail rule. A statement such as “easy to read” is not a reliable inspection criterion; measurable requirements might instead specify the visible color contrast, viewing angle, segment alignment, or legibility under defined lighting.
Approved drawings and a signed reference sample help prevent different interpretations between product development, the factory, and the buyer. Record critical dimensions, color references, material requirements, surface finish, label content, and firmware or configuration versions where relevant. Any approved change to a component, mold, display, supplier, or production process should trigger a documented review, since an apparently minor substitution can affect fit, battery life, appearance, or calibration.
Inspect incoming materials and critical components
Incoming inspection should focus on parts that can create high-impact failures or are difficult to detect after assembly. Depending on the design, these may include the display lens, colored timing element, printed scale, buttons, circuit board, buzzer, battery contacts, housing resin, and packaging. Verify part identity against approved specifications and check for damage, contamination, dimensional variation, incorrect color, poor printing, or inconsistent finish. Supplier certificates and inspection records can support review, but they do not replace risk-based verification of the actual lot.
For components with measurable performance, establish a sampling method and retain results by supplier lot. A visual disk that is warped or misaligned, for example, may rub against its cover and produce uneven movement. A poorly formed battery contact can create intermittent operation that is difficult to reproduce in a brief final test. Early detection reduces the cost of rework and helps the factory isolate a supplier issue before affected parts are assembled into finished products.
Use lot sampling with clear acceptance rules
Inspection sampling is useful when checking every unit is impractical, but it is not a substitute for defining the risk. The ISO 2859-1 standard describes sampling schemes indexed by acceptance quality limit for lot-by-lot inspection by attributes. Buyers and suppliers should agree on the applicable plan, inspection level, defect classifications, and acceptance and rejection numbers rather than relying on an unexplained “AQL passed” statement. Sampling reduces inspection workload; it does not guarantee that every unit in an accepted lot is defect-free.
Classify defects according to customer and safety impact. A missing required warning or a unit that fails to start may merit a different response from a minor cosmetic mark that does not affect use. Specify critical, major, and minor categories in the quality agreement, then define escalation rules for repeated failures, borderline results, and suspected systemic defects. For high-risk functions, combine lot sampling with targeted 100% checks at the relevant production station.
Verify timing, display behavior, and operating reliability
Functional testing should reflect how the product will be used, not merely whether it powers on. A visual countdown timer may serve classrooms, offices, clinics, kitchens, or home productivity routines, and each use case can place different demands on readability, controls, alarms, and handling. A repeatable test method enables a buyer to compare pilot samples with production units and helps the factory detect process drift before it becomes a shipment-wide problem.
Measure countdown accuracy across the operating range
Test representative settings near the low end, middle, and upper end of the product’s timing range. Use a calibrated reference clock or time-measurement instrument, record the selected duration and actual elapsed time, and compare the result with the product’s declared tolerance. Include start, stop, pause, reset, and restart behavior where those functions are part of the design. The test procedure should define whether timing begins at button activation, after a display transition, or following another product-specific event.
Repeatability matters as much as a single passing result. Run repeated cycles on sampled units and compare results across units, shifts, and production lots. If performance changes after a battery replacement, a reset, or a particular control sequence, record that condition rather than dismissing it as user error. Where the design depends on electronic timing, validate the relevant component and firmware configuration; where it includes a moving visual indicator, inspect the mechanism throughout its travel for sticking, wobble, or inconsistent movement.
Check visibility, controls, sound, and power behavior
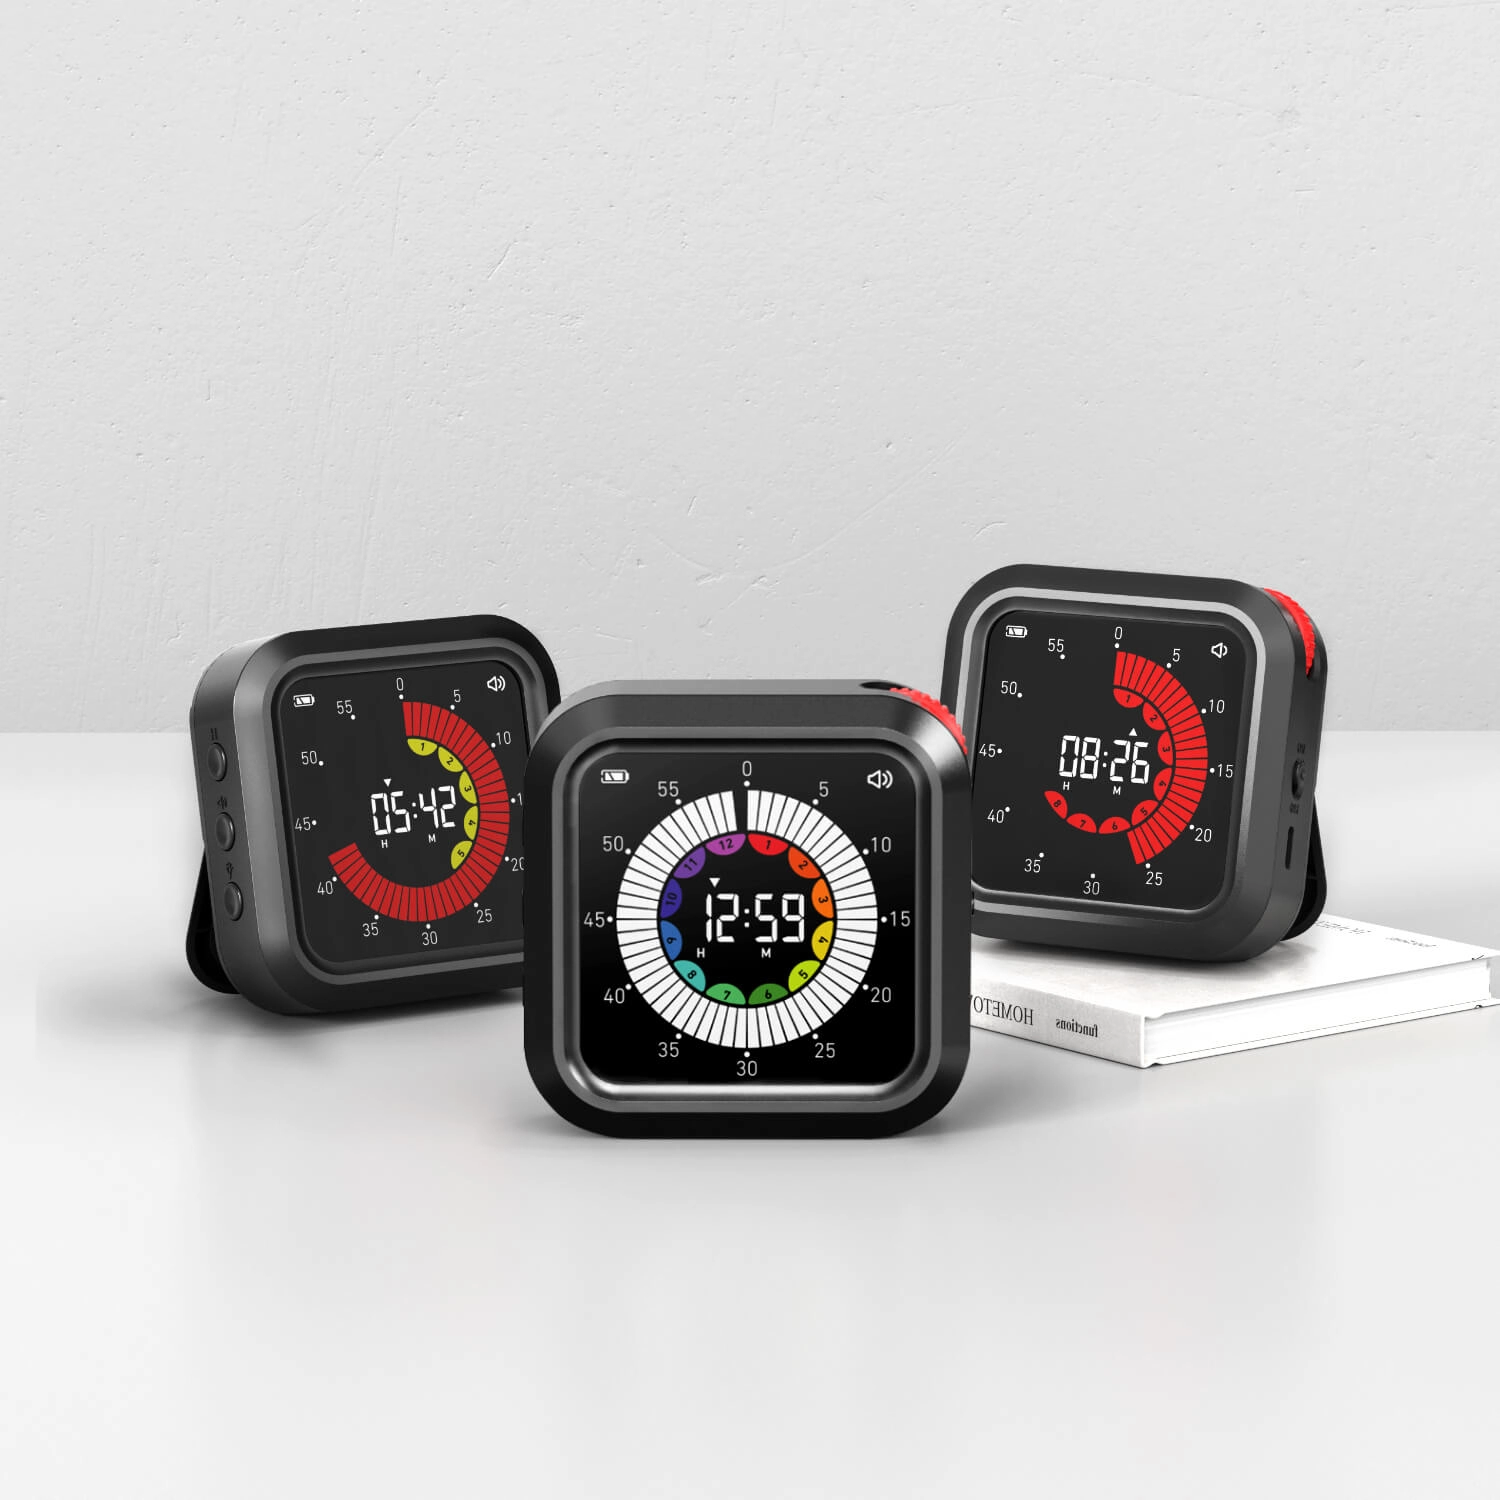
Inspect the display at the angles and distances likely in the intended environment. Confirm that the remaining-time area is easy to distinguish from the elapsed area, color boundaries are correctly placed, and markings do not obscure the indicator. Check that controls respond consistently without excessive force, unintended double activation, or loose movement. For an audible alert, verify activation and consistency using a defined distance and test environment; where sound level is a requirement, use an appropriate meter and document the method rather than relying only on subjective judgment.
Power checks should cover the specified battery type or power input, polarity protection where applicable, low-battery indication if included, and operation during the expected use cycle. Examine battery contacts for secure retention and corrosion risks, and confirm that the housing closes correctly without pinching wires or interfering with controls. A brief power-on test alone may not reveal intermittent contacts or premature battery depletion, so test duration and sample selection should reflect the product’s intended service pattern.
Use standards appropriately and compare test methods
Standards can structure a test program, but they should be selected for the specific product and market rather than cited as generic proof of quality. The IEC 60068-2-1 environmental testing method addresses tests for cold conditions; relevant environmental methods may help assess whether a timer continues to operate after defined exposure. Electrical and electronic products also require a market-specific review of applicable safety requirements. The IEC 62368-1 standard addresses safety for audio/video, information, and communication technology equipment; a supplier should confirm applicability with the responsible compliance professional rather than assume every timer falls within its scope.
| Factory check | What it establishes | Practical limitation |
|---|---|---|
| 100% functional station test | Confirms each unit completes the defined basic operations at the point tested. | Does not by itself establish long-term durability or performance outside the tested sequence. |
| Lot sampling by attributes | Supports consistent acceptance or rejection decisions for a defined production lot and defect classification. | An accepted sample does not mean every unit in the lot is defect-free; the plan and acceptance rules must be stated. |
| Environmental exposure test | Evaluates specified performance after controlled exposure to conditions such as cold or heat. | Results apply only to the selected conditions, duration, sample, and acceptance criteria. |
| Instrument calibration and traceability review | Provides evidence that measurement results are linked to recognized references through a documented calibration chain. | Traceability does not automatically mean an instrument is suitable for every measurement or tolerance. |
Environmental test severity should follow the product specification, expected distribution and storage conditions, and target market. The NIST explanation of metrological traceability describes the importance of a documented, unbroken chain of calibrations to specified references. In practice, buyers should request instrument identification, calibration status, and measurement records for critical checks. A calibrated device improves confidence in results only when the test method, resolution, and measurement uncertainty are appropriate to the tolerance being evaluated.
Turn inspection results into stronger supplier and brand outcomes
Factory checks deliver value when they are linked to release decisions and corrective action. A test report that records only “pass” provides little insight into trends, recurring failures, or the lot’s actual performance. Ask for results that identify the production date or lot, inspected quantity, defect category, measured values where applicable, test equipment, and disposition. This evidence gives procurement, quality, and product teams a shared basis for deciding whether to release, rework, hold, or investigate a shipment.
Define nonconformance handling before production
A quality agreement should set out how the supplier contains suspect stock, notifies the buyer, investigates root cause, and verifies corrective action. When a defect appears, the response should distinguish immediate containment from permanent prevention. For example, replacing a defective control may resolve affected units, while a process review may be needed to correct the assembly fixture or component tolerance that caused the failure. Require effectiveness checks on subsequent production rather than closing an issue solely because a corrective-action form was submitted.
Pre-shipment inspection can confirm finished-product condition, quantity, packaging, labeling, and selected function tests, but it is only one layer of control. Pilot builds, first-article approval, in-process audits, and post-market feedback help reveal issues that a final sample may miss. Buyers should align inspection timing with production milestones so there is enough time to address a problem without delaying the shipment or approving an unverified workaround.
Connect quality controls to product range and production planning
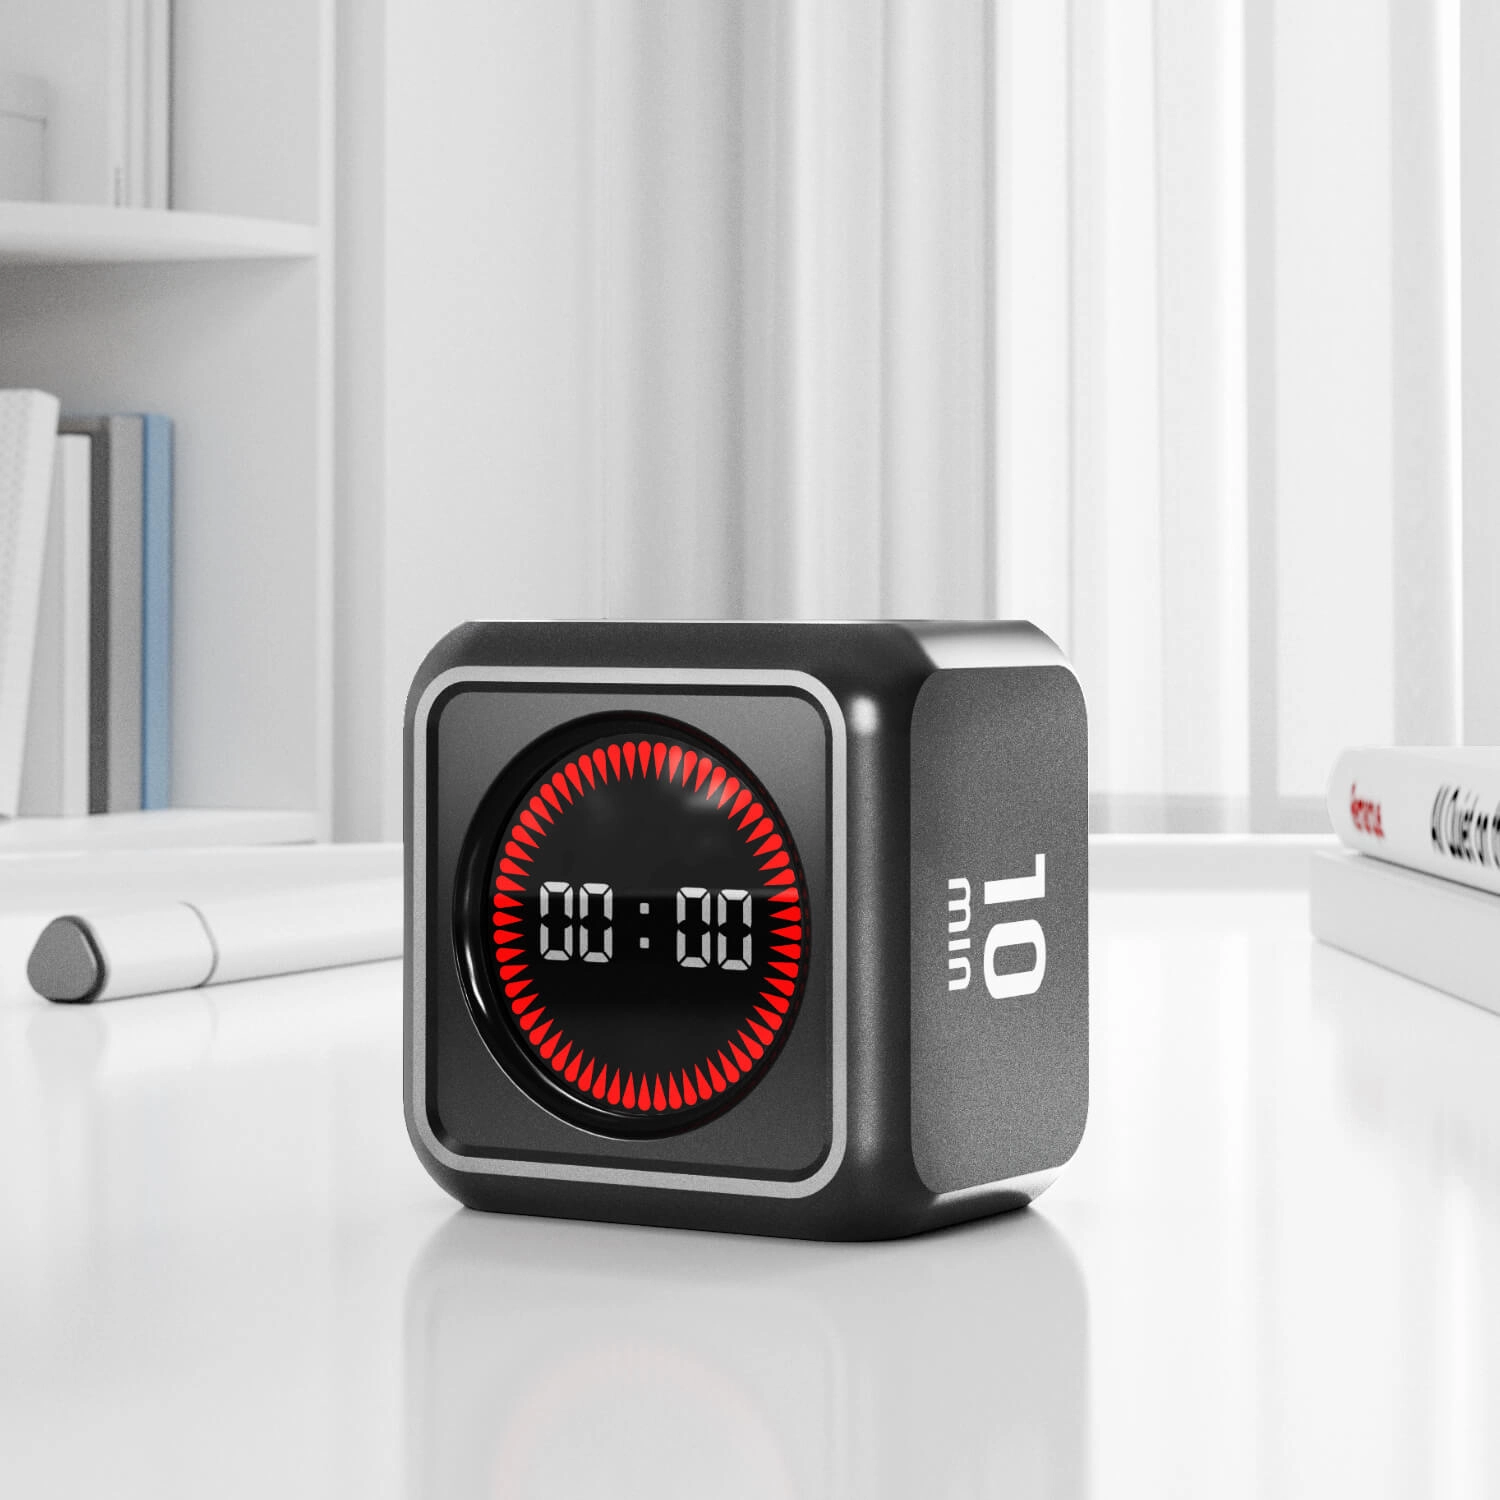
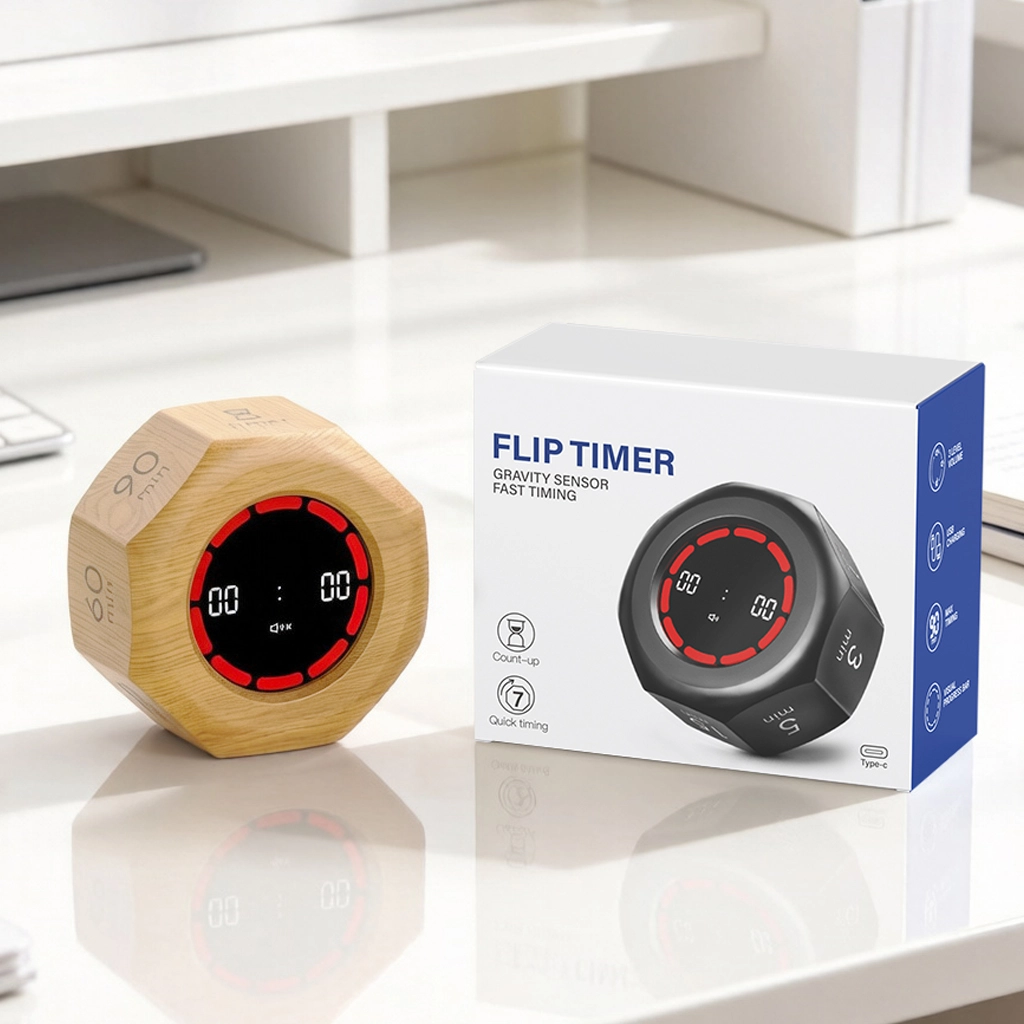
Our product portfolio includes digital timers and Pomodoro timers, as well as thermo-hygrometers and temperature-humidity monitors. These products serve different measurement and user needs, but dependable quality across a range still relies on clear specifications, controlled components, repeatable assembly, and appropriate functional verification. For a visual countdown model, the plan should give particular attention to indicator movement, readability, timing tolerance, and control behavior; for environmental monitoring products, measurement accuracy and sensor-related checks require their own defined methods.
Our team can align the inspection plan with the selected configuration, market requirements, packaging, and buyer acceptance criteria before production release. That alignment helps prevent specification gaps from surfacing during final inspection and gives both parties a practical record for reviewing changes and resolving nonconformances. Rather than treating a certificate or a single audit as a complete quality guarantee, buyers should assess whether the supplier can provide applicable documentation, test evidence, calibrated measurement practices, and a clear process for managing production changes.
Evaluate the evidence behind every quality claim
During supplier qualification, request a sample control plan, a completed inspection report, and an example of a corrective-action record with sensitive commercial information removed. Check that the procedures identify acceptance limits rather than vague goals and that recorded results correspond to the actual product revision. Confirm whether inspections are performed by trained personnel, how nonconforming product is segregated, and how inspection equipment is maintained. Where a supplier uses subcontractors for components or testing, clarify which party owns the records and who is responsible for resolving failures.
For procurement teams, the strongest quality case combines product samples, documented factory controls, and transparent communication. A consistent visual timer can reduce customer complaints, returns, replacement shipments, and reputational risk, but those business outcomes depend on how well requirements are implemented and verified. Clear criteria established before the purchase order make performance easier to measure, help the factory prioritize critical characteristics, and support a more predictable launch.
Contact our team to discuss timer specifications, factory inspection requirements, or the digital timer and environmental-monitoring products best suited to your program.
Frequently Asked Questions
What quality checks should a factory perform on a visual timer?
A practical control plan covers incoming components, timing accuracy, display alignment and readability, control response, alarm behavior, power performance, assembly, and packaging. It should define test conditions, measurable acceptance criteria, records, and actions for nonconforming results.
How can buyers verify visual timer accuracy?
Test settings near the low, middle, and upper ends of the timing range with a calibrated reference clock or time-measurement instrument. Record selected and actual elapsed times, compare results with the declared tolerance, and repeat cycles on representative units.
Does an accepted inspection sample prove that every timer in a lot is defect-free?
No. Lot sampling supports a defined acceptance decision but does not establish that every unit is defect-free. Buyers and suppliers should agree on the sampling plan, inspection level, defect categories, and acceptance and rejection numbers.
Which standards may be relevant to factory testing?
ISO 2859-1 describes sampling schemes for lot-by-lot inspection by attributes. IEC 60068 environmental methods may apply to specified exposure testing, while IEC 62368-1 addresses safety for certain audio/video, information, and communication technology equipment. Applicability depends on the product and target market and should be confirmed by a qualified compliance professional.
What records should buyers request from a timer supplier?
Request lot-identified inspection reports, actual measurements where relevant, defect classifications, test-equipment identification and calibration status, product revision details, and documented nonconformance and corrective-action procedures. These records help assess whether quality claims are supported by repeatable evidence.
Why are calibration and measurement traceability important?
Traceability provides a documented link between measurement results and specified references. It supports confidence in test data when the instrument, method, resolution, and measurement uncertainty are suitable for the product tolerance.
Top room temperature meter Manufacturers and Suppliers
Digital Visual Countdown Timer Certifications and Compliance Standards Buyers Should Check
Top 10 desk clock with timer and alarm manufacturers and suppliers
Best Indoor Room Thermometers: Buyer's Guide 2026
Interested in this article?
Let’s talk.
Need specifications, pricing, or customization options? We’ll provide everything you need.

Youben life
Youben life