Private Label Pomodoro Timer Quality Control: Production Checks That Protect Your Brand
- Building a Quality Framework for Focus-Timer Hardware
- Translate the product brief into measurable specifications
- Use stage-gate approvals instead of one final inspection
- Set sampling rules and defect classifications
- Production Checks That Prevent Functional and Cosmetic Failures
- Inspect components before assembly
- Verify assembly, firmware, and timing performance
- Test the display, sound, power system, and enclosure
- Compliance, Reliability, and Shipment Release Controls
- Separate compliance evidence from marketing claims
- Build reliability testing around actual use
- Control the final lot and the documentation package
- Why an Integrated OEM Partner Strengthens Brand Protection
- Engineering control from concept through tooling
- Compliance and scalable manufacturing for market launch
- Turn quality data into commercial value
- Frequently Asked Questions
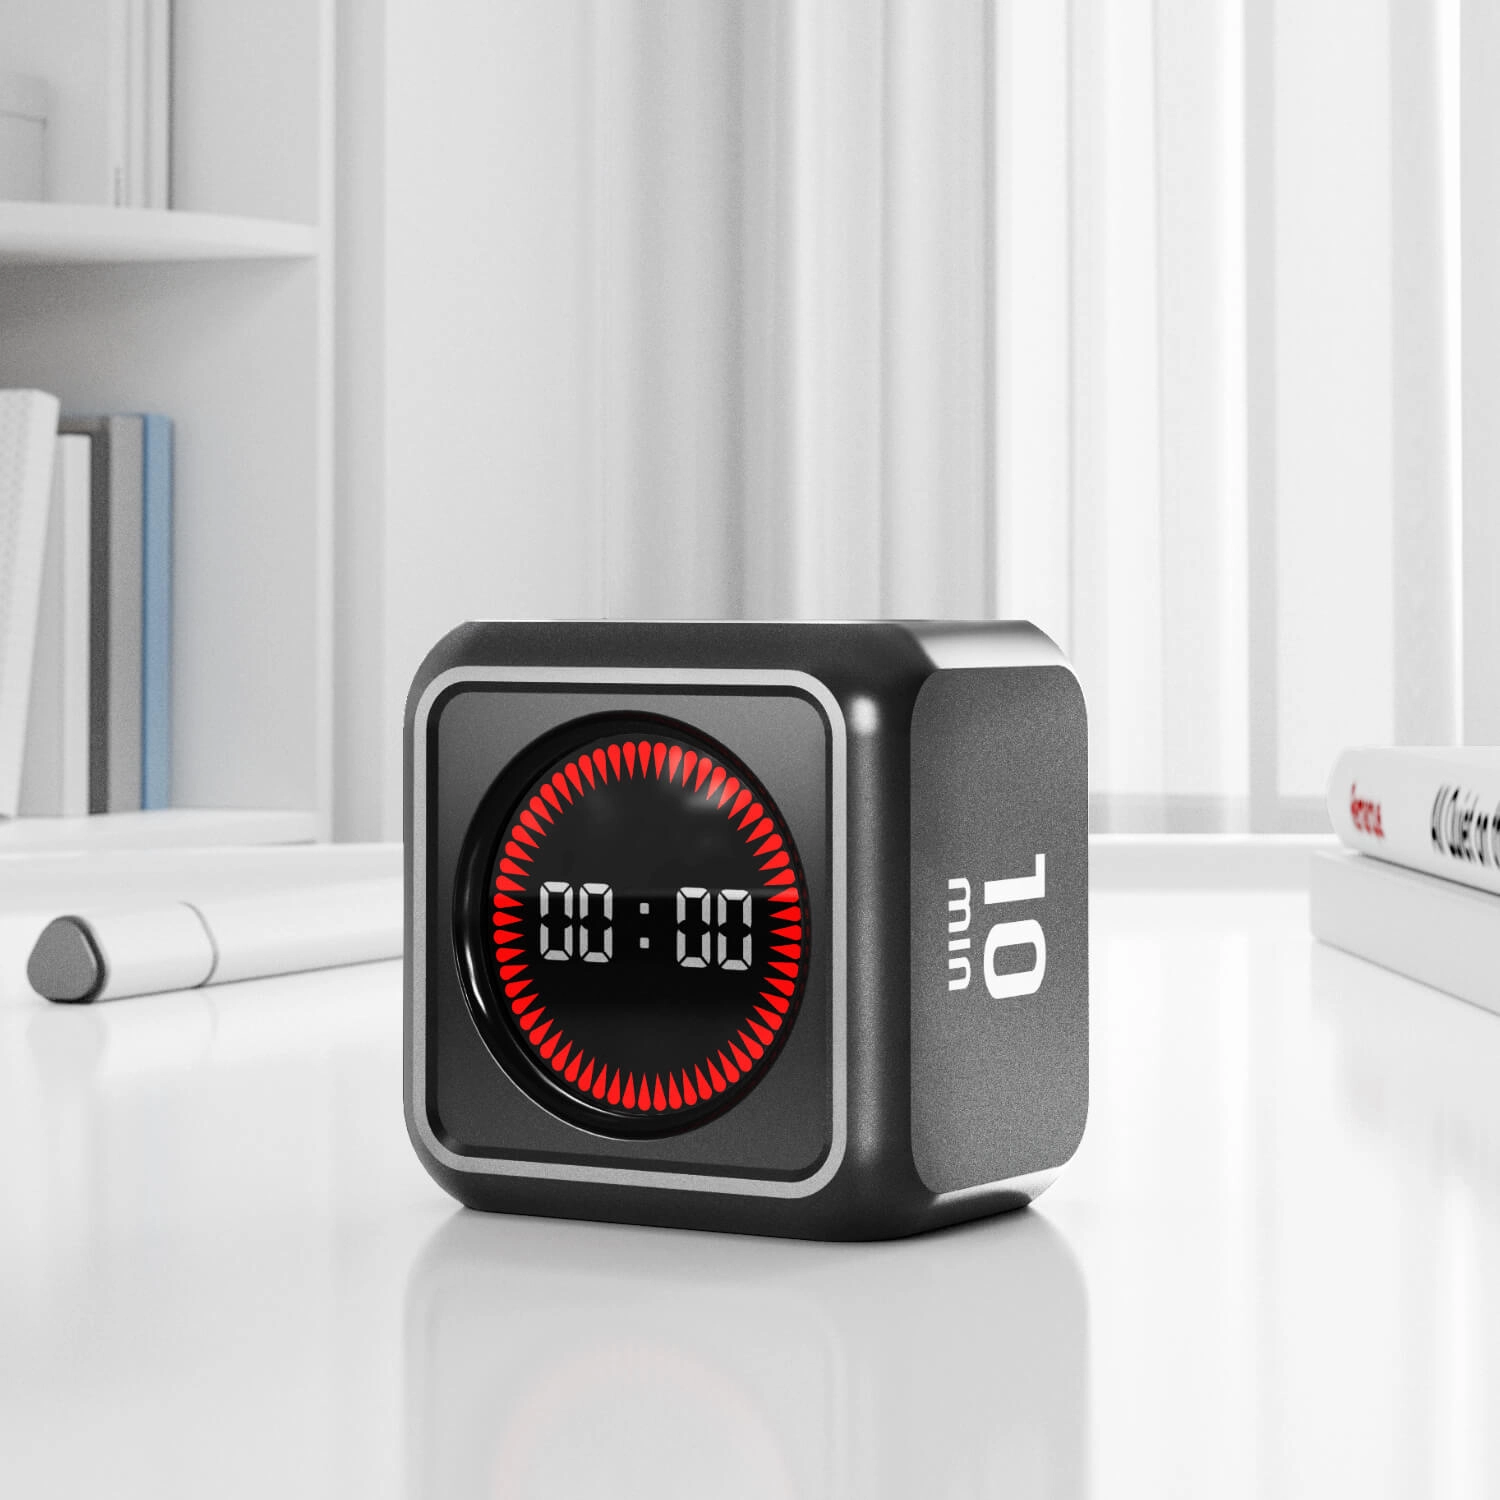
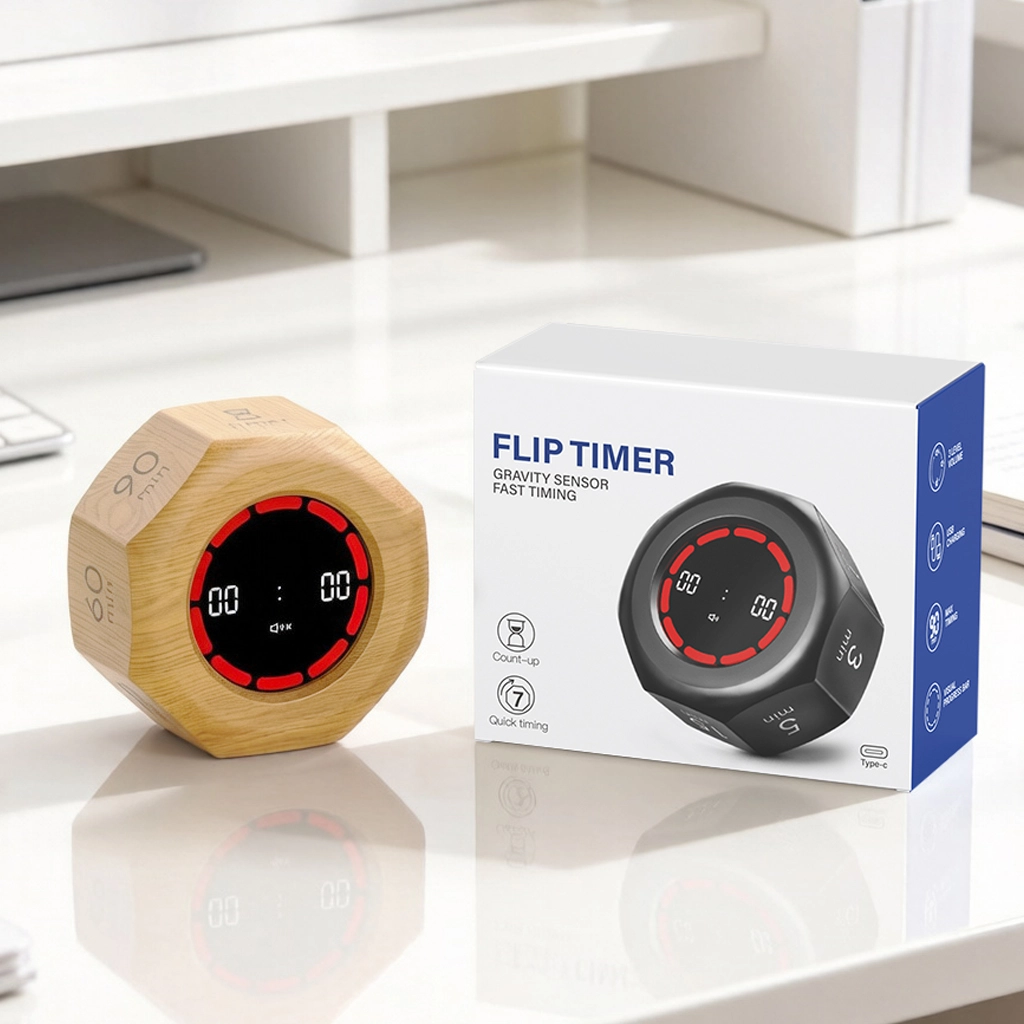
A successful private label Pomodoro timer program requires a documented quality system that protects timing accuracy, user safety, retail presentation, and long-term brand reputation. The most effective approach combines approved specifications, first-article validation, incoming material inspection, in-process control, final random inspection, firmware verification, battery and electrical safety testing, regulatory compliance, and packaging audits. For buyers sourcing a Digital Timer, production quality should be measured through objective acceptance criteria rather than visual inspection alone. A supplier should be able to demonstrate traceability from component purchasing and custom mold tooling through assembly, calibration, reliability testing, and shipment release.
Building a Quality Framework for Focus-Timer Hardware
Translate the product brief into measurable specifications
Quality control begins before tooling or mass production. The product brief should define countdown ranges, work and break presets, alarm duration, sound levels, display visibility, button response, battery type, charging method, standby behavior, memory retention, dimensions, surface finish, logo placement, and packaging requirements. Ambiguous terms such as “large display,” “quiet alarm,” or “High Quality feel” create disputes because different teams interpret them differently. A stronger specification converts each expectation into a measurable requirement, such as a minimum character height, a maximum timing deviation, a defined key travel, or an approved color reference.
For a branded study timer, user experience is part of product quality. The control layout should make it difficult to start the wrong mode, accidentally reset a session, or miss the end-of-cycle notification. The interface should also account for users working in classrooms, offices, kitchens, and home environments. Buyers should approve physical samples and firmware behavior together because a casing revision, button geometry change, or display update can alter the perceived performance of the finished unit.
Use stage-gate approvals instead of one final inspection
A stage-gate model reduces the cost of late discovery. Recommended gates include design review, engineering validation, design validation, production validation, and shipment release. At each gate, the project owner should receive evidence rather than assurances: drawings, bill of materials, software revision records, test reports, golden samples, defect photographs, and corrective-action status. The approved golden sample must be physically controlled and identified by revision so that factory inspectors, buyers, and third-party laboratories compare production against the same reference.
An ISO 9001-aligned quality management approach is useful because it emphasizes documented processes, customer requirements, corrective action, and continual improvement. The International Organization for Standardization’s ISO 9001 overview explains the role of a quality management system in consistently delivering products that meet customer and regulatory requirements. ISO 9001 certification does not automatically prove that every unit is defect-free, but a mature system makes responsibilities, records, escalation, and process control easier to verify.
Set sampling rules and defect classifications
Inspection plans should define sample size, inspection level, acceptable quality limits, and the response to critical, major, and minor defects. A critical defect can involve unsafe charging, exposed conductive parts, overheating, or a battery fault. A major defect may include a nonfunctional timer, incorrect firmware, a broken display segment, or a housing that cannot close correctly. Minor defects can include small cosmetic marks that remain within the approved visual standard. Buyers should avoid relying on a supplier’s informal phrase “passed inspection”; the report should state what was checked, how many units were sampled, and which acceptance criteria were applied.
Production Checks That Prevent Functional and Cosmetic Failures
Inspect components before assembly
Incoming quality control should cover circuit boards, integrated circuits, displays, buttons, speakers, batteries, USB cables, magnets, plastic housings, labels, and printed materials. Component checks should verify part numbers, quantities, dimensions, color, surface finish, and revision status against the approved bill of materials. Electronic components should be screened for visible damage, solder contamination, missing parts, and inconsistent labeling. For molded parts, inspectors should look for short shots, sink marks, warpage, flash, flow lines, stress whitening, and color variation.
Custom branding introduces additional risks. A logo can be reversed, positioned incorrectly, printed with the wrong ink, or applied at an inconsistent depth. Artwork approval should therefore include a dimensioned placement drawing, color reference, minimum line thickness, and an approved physical sample. Packaging artwork needs the same discipline, especially where product claims, battery symbols, importer details, language translations, or recycling marks vary by market.
Verify assembly, firmware, and timing performance
In-process inspection should confirm that circuit boards are seated correctly, wires are routed safely, screws are tightened consistently, battery connectors are secure, and buttons operate without binding. Functional testing should then verify power-on behavior, mode selection, countdown and count-up functions, pause and resume logic, alarm output, brightness settings, low-battery indication, automatic sleep, memory retention, and reset behavior. Every firmware revision should have a controlled release number. A factory should not be allowed to substitute software because a later version appears similar; even a small change can affect timing logic, standby current, language strings, or button mapping.
Timing accuracy is a central brand promise. Testing should compare the device against a calibrated reference over a defined period and under representative operating conditions. The acceptance requirement must state the permitted deviation, test duration, starting condition, and whether the result applies to every unit or a statistical sample. Buyers should also check whether the timer continues accurately during low battery, after repeated pause-and-resume cycles, and following a power interruption.
Test the display, sound, power system, and enclosure
Display inspection should cover all segments, icons, brightness levels, viewing angles, flicker, dead pixels, uneven illumination, and contrast under bright and low-light conditions. Acoustic testing should verify that the alarm is audible at the intended distance without exceeding the product’s positioning requirements. If a silent or vibration mode is offered, the mode must be checked for reliable activation and clear user feedback.
Battery-powered products require more than a charge-and-discharge demonstration. The production test plan should address charging behavior, overcurrent protection, abnormal charging response, connector retention, battery swelling risk controls, operating temperature, and idle current. The exact test program depends on the battery chemistry, power architecture, and destination markets. Electrical and electronic equipment placed on the European market may also require evidence supporting applicable conformity obligations; the European Commission guidance on CE marking clarifies that the mark indicates a manufacturer’s declaration that relevant EU requirements have been met, not a universal quality seal.
Enclosure testing should simulate the handling that occurs in distribution and everyday use. Useful checks include button-cycle testing, USB insertion and removal, drop testing from an agreed height, scratch and abrasion evaluation, label adhesion, stand stability, and housing seam inspection. A test is meaningful only when the method, equipment, sample count, pass criteria, and post-test inspection are recorded.
| Production checkpoint | Typical evidence | Brand risk controlled |
|---|---|---|
| Incoming component inspection | Part-number verification, dimensional records, visual report | Wrong components, cosmetic inconsistency, assembly stoppage |
| First-article approval | Approved sample, drawings, firmware revision, golden sample | Uncontrolled design changes and specification disputes |
| In-process functional testing | Test fixtures, operator records, defect logs | Nonfunctional units reaching final assembly |
| Reliability and safety testing | Drop, cycle, charging, temperature, and electrical reports | Premature failure, unsafe operation, warranty claims |
| Final random inspection | Sampling plan, defect classification, photos, release decision | Mixed lots, packaging errors, shipment-wide quality issues |
Compliance, Reliability, and Shipment Release Controls
Separate compliance evidence from marketing claims
Buyers should request a product-specific compliance file rather than accepting generic certificates from a supplier. The file may include declarations of conformity, test reports, material declarations, safety assessments, electromagnetic compatibility results, battery documentation, and restricted-substance evidence. RoHS requirements restrict certain hazardous substances in electrical and electronic equipment in the European Union; the European Commission RoHS information provides the governing context. A supplier should identify the tested model, hardware revision, laboratory, test standard, date, and applicable market so that buyers can assess whether the evidence matches the actual product.
For products that contain digital electronics, electromagnetic compatibility deserves specific attention. A timer that performs correctly in isolation may create interference or behave unpredictably near other equipment if the design is not properly controlled. The U.S. Federal Communications Commission EMC resources explain the broader regulatory context for electromagnetic compatibility and equipment authorization. Market-specific obligations should be reviewed by the importer, brand owner, and qualified compliance professionals before launch.
Build reliability testing around actual use
Reliability testing should reflect the product’s expected lifecycle rather than relying only on a short functional check. A practical program can include repeated button actuation, repeated alarm cycles, charging cycles, power-on and power-off cycles, stand loading, display operation, storage at defined temperature and humidity conditions, and transportation simulation. The correct limits depend on the product design and market positioning, but the important procurement question is whether the supplier has converted expected use into repeatable tests.
Failure analysis is equally important. When a unit fails, the supplier should isolate the failure mode, identify the root cause, define containment, implement corrective action, and verify effectiveness. A replacement shipment without root-cause analysis may temporarily reduce complaints while leaving the underlying defect active. Buyers should review corrective-action reports for evidence that the change was applied to all affected work-in-progress and finished goods.
Control the final lot and the documentation package
Shipment release should occur only after quantity reconciliation, product inspection, carton drop or handling checks where required, barcode verification, accessory confirmation, and packaging review. Each carton should identify the model, lot, quantity, destination information, and handling marks required by the logistics plan. The final report should include production dates, inspection results, deviations, rework quantities, and approval signatures.
Digital records are especially valuable for marketplace brands and distributors managing returns across several channels. Serial numbers or lot codes can connect customer complaints to a production batch, firmware revision, battery supplier, or packaging date. This traceability supports faster containment and more credible communication with retailers, regulators, and end users.
Why an Integrated OEM Partner Strengthens Brand Protection
Engineering control from concept through tooling
We established Youben life in 2010 as an OEM/ODM manufacturer dedicated to Digital Timers, Pomodoro timers, Visual Countdown Clocks, temperature and humidity monitors, and thermo-hygrometers. Our 20,000m² vertically integrated facility in Guangzhou, China supports turnkey development for global brands and Amazon bestsellers. This structure allows our team to connect industrial design, mechanical design, electronics, firmware, tooling, assembly, inspection, and packaging decisions instead of treating quality as a final-line activity.
Our R&D capabilities include ID/MD industrial design, custom IC programming, precision mold tooling, prototype development, firmware control, and retail-ready packaging. For a branded focus timer, this integration helps reduce handoff errors between design agencies, electronic suppliers, mold factories, assemblers, and packaging vendors. It also gives project owners a clearer route for resolving issues such as button feel, display readability, enclosure strength, alarm behavior, and visual differentiation.
Compliance and scalable manufacturing for market launch
Our quality and compliance process is designed to support products meeting strict CE, FCC, and RoHS requirements, subject to the applicable product configuration and destination-market assessment. We maintain a decade of engineering experience and scalable production capacity so that a validated design can move from pilot quantities to larger commercial orders without abandoning the original inspection logic. That continuity matters to distributors and brand owners because uncontrolled scale-up can introduce alternate materials, revised firmware, inconsistent molding, or packaging substitutions.
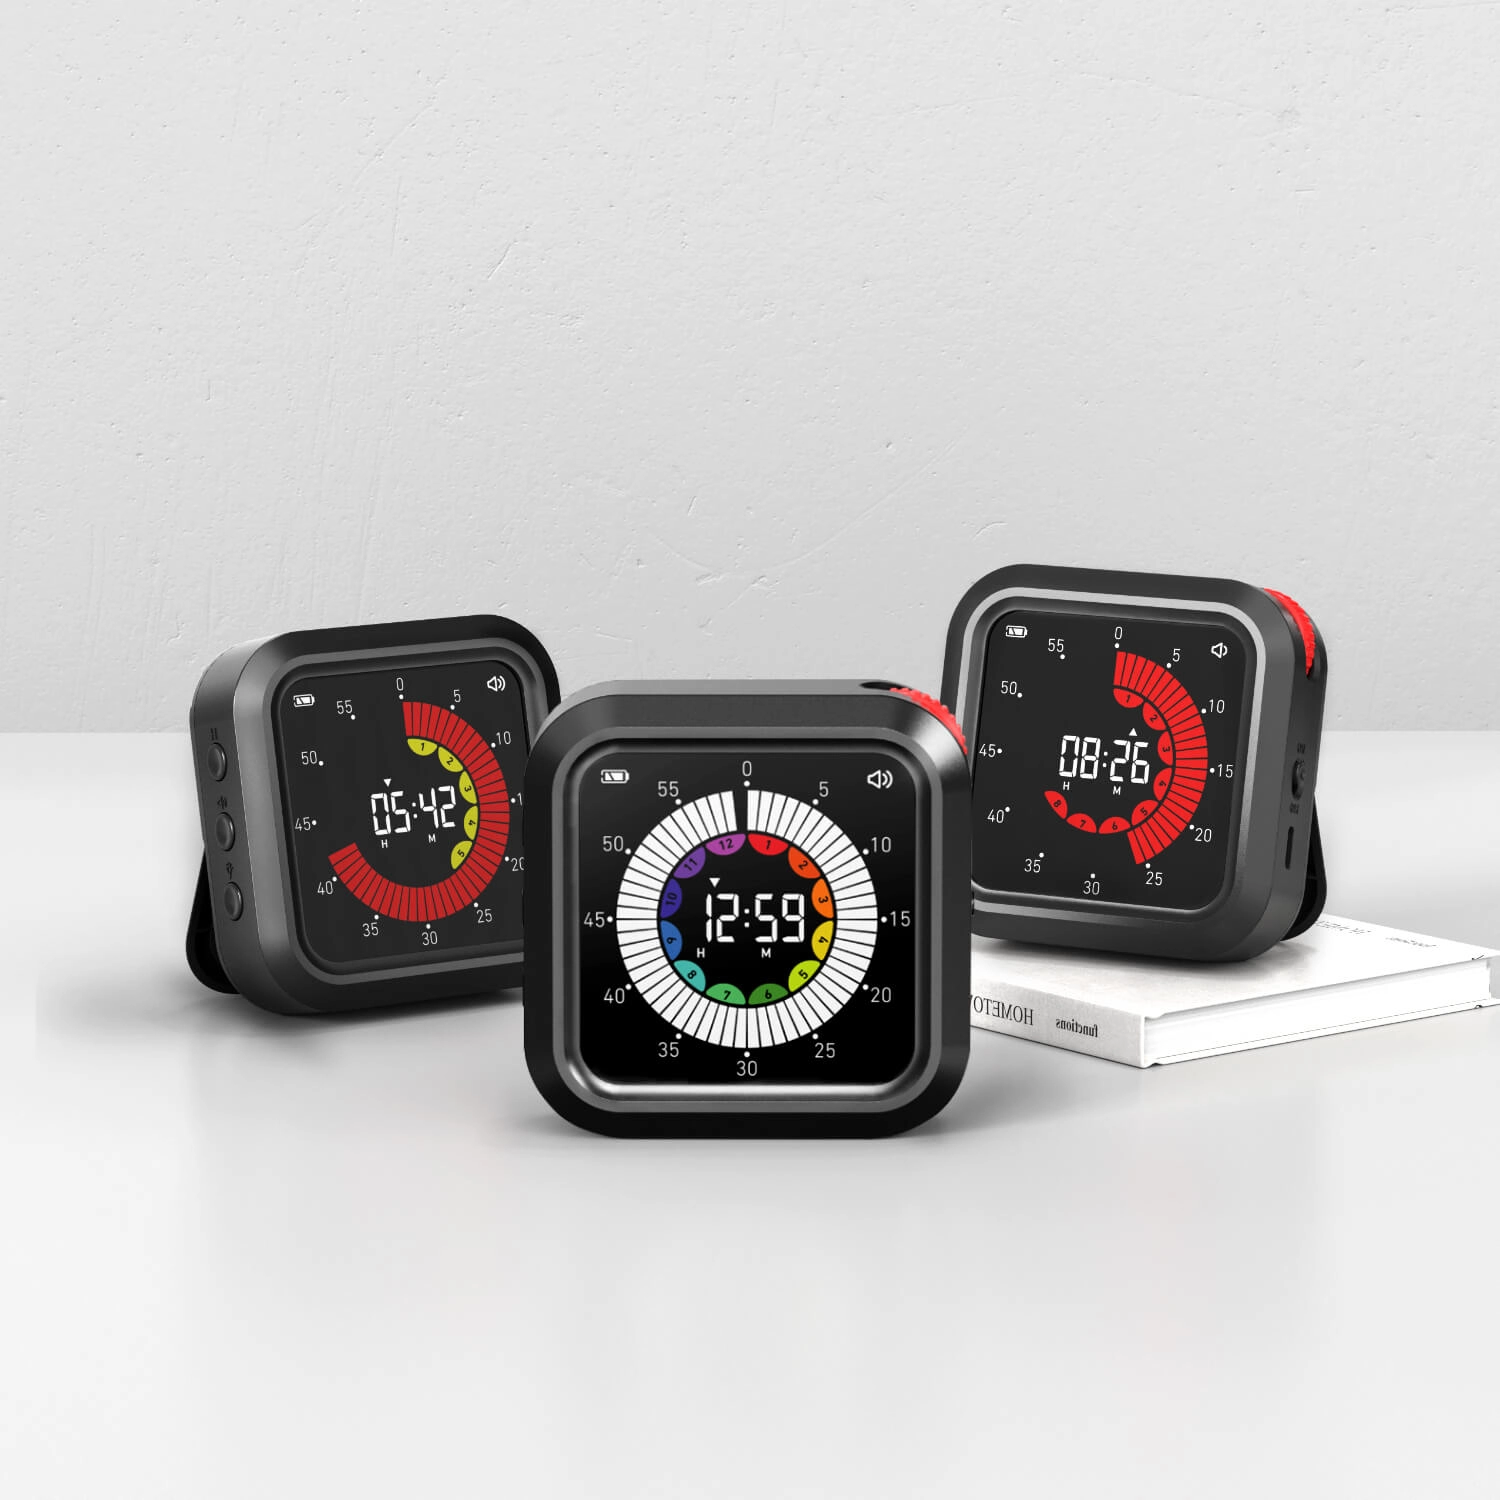
Our product scope includes Digital Timer solutions for education, productivity, cooking, sports, and commercial operations, along with Pomodoro timer formats, Visual Countdown Clocks, thermo hygrometer products, and temperature humidity monitors. Each category requires different performance priorities: a study timer may emphasize silent operation and intuitive controls, while a temperature humidity monitor may require sensor stability, calibration control, and clear environmental readings. A capable OEM partner should adapt the quality plan to the application instead of applying one generic checklist to every device.
Turn quality data into commercial value
Quality control protects more than factory yield. It reduces marketplace returns, prevents negative reviews, lowers warranty handling costs, protects advertising investment, and gives retail buyers confidence in replenishment. Consistent color, accurate timing, dependable power, and complete documentation also help a differentiated product maintain its price position. Our team works with project owners on product definition, engineering validation, manufacturing, compliance coordination, and retail packaging so that quality decisions support both technical performance and brand identity.
For procurement teams comparing suppliers, the most useful evaluation is evidence-based: examine the facility, ask how revisions are controlled, review sample inspection reports, confirm test equipment, assess corrective-action discipline, and verify that compliance documents match the intended model. The lowest quoted unit price is rarely the lowest total cost when defects generate returns, relabeling, emergency freight, or lost channel trust.
Contact Youben life at info@youbenlife.com or visit our Digital Timer product portfolio to discuss a quality-controlled OEM/ODM program for your next branded timer or environmental monitoring product.
Frequently Asked Questions
What should be included in a quality plan for a branded Pomodoro timer?
The quality plan should define approved specifications, component inspection, first-article approval, firmware control, in-process testing, timing accuracy, display and alarm checks, battery and charging safety, reliability testing, final sampling, packaging inspection, and shipment-release documentation.
How can buyers verify timing accuracy before mass production?
Buyers should compare the device with a calibrated reference over a defined test period and record the permitted deviation, starting condition, operating mode, and environmental conditions. The same requirement should be checked during pilot production and final inspection.
What compliance documents should a timer manufacturer provide?
A supplier should provide product-specific compliance evidence such as declarations of conformity, applicable test reports, material declarations, electromagnetic compatibility results, battery documentation, and restricted-substance evidence. The documents should identify the tested model, hardware revision, laboratory, date, and destination market.
Why is firmware revision control important for a digital timer?
Firmware controls timing logic, button functions, alarm behavior, standby current, language strings, and memory behavior. A controlled revision process prevents an unapproved software change from creating inconsistent performance across production batches.
What defects are considered critical in timer production?
Critical defects can include unsafe charging, exposed conductive parts, overheating, battery faults, or other conditions that may create a safety risk. These issues should trigger immediate containment and shipment suspension until the root cause and corrective action are verified.
How does an integrated OEM/ODM manufacturer reduce quality risk?
An integrated manufacturer connects industrial design, electronics, firmware, tooling, assembly, testing, and packaging under coordinated process control. This reduces handoff errors, improves revision traceability, and makes it easier to apply corrective actions across the complete product system.
Best Smart Focus Timers for Remote Teams and Offices
Custom Pomodoro Timer Manufacturer: Branding, Design, Functions, and Packaging Options
Use Cases: Smart Focus Timers for Offices, Schools, Gyms
Smart Focus Timer ROI: Measuring Productivity Gains
Interested in this article?
Let’s talk.
Need specifications, pricing, or customization options? We’ll provide everything you need.

Youben life
Youben life